


Pharmaceutical Cold Room Design and Supply
A pharmaceutical cold room is an insulated, temperature-controlled space for products with defined storage requirements. TunelGroup designs and supplies cold-room panels, doors and refrigeration systems around the product specification, room capacity and conditions at your facility.
Share your required temperature range, internal room dimensions, storage quantity and project location. These details form the basis of a coordinated proposal for the room envelope, refrigeration equipment and requested controls.
Why Pharmaceutical Cold Storage Requires Careful Planning
Effective storage starts with the product manufacturer’s instructions and your operating procedures. Room dimensions alone do not define the cooling duty or the conditions experienced by stored products.
- Product requirements: establish the permitted temperature range, packaging and any humidity limits before selecting equipment.
- Storage capacity: plan shelf or pallet positions, access aisles and clearances around stored goods.
- Daily operation: account for incoming product temperature, loading frequency and door openings.
- Verification: agree monitoring, acceptance tests and documentation with the team responsible for the facility.
TunelGroup Pharmaceutical Cold Room Solutions
Define the storage conditions for each product group. A shared room should only be considered where the product requirements and operating procedures are compatible.
| Application | Temperature basis | Humidity basis | Design considerations |
|---|---|---|---|
| Refrigerated medicines | Manufacturer’s labelled storage range | Product and packaging requirements | Storage quantity, door traffic, airflow and monitoring |
| Vaccines and biologics | Specification for the particular product | As required by the product specification | Handling procedures, excursions and alarm response |
| Laboratory materials | Approved laboratory storage protocol | Material-specific requirements | Storage format, segregation and recording requirements |
| Pharmaceutical raw materials | Supplier’s approved storage instructions | Material and packaging requirements | Room zoning, product movement and cleaning access |
| Frozen pharmaceutical products | Exact range specified by the product owner | As specified for the application | Dedicated refrigeration selection and project review |
| Distribution storage | Storage requirements of the handled products | As required for the stored products | Receiving, dispatch, loading peaks and usable capacity |
Features of a Project-Specific Pharmaceutical Cold Room
- Insulated panels: wall, ceiling and floor construction selected for the room conditions, site and loading requirements. Explore our cold room panels.
- Door and access arrangement: hinged or sliding access, opening size and handling clearances coordinated with the storage layout. See cold room doors.
- Refrigeration equipment: system capacity assessed using product load, room heat gains, ambient conditions and the operating schedule.
- Air distribution: evaporator position and storage clearances considered together so the agreed storage area can be assessed under operating conditions.
- Controls: operating setpoints and requested monitoring, recording and alarm functions defined in the technical proposal.
- Maintainability: service access, cleaning access and component placement considered during layout planning.
Visual Insights into Pharmaceutical Cold Storage
Application illustrations from our existing pharmaceutical cold-room page. The final room layout and equipment are defined for each project.
Pharmaceutical Cold Room

An insulated room layout for temperature-controlled pharmaceutical storage.
Specialist Storage Applications
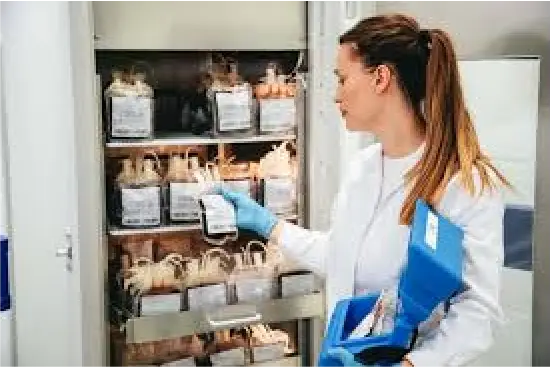
Specialist products require their own confirmed storage conditions and equipment specification.
Biologics Storage Layout
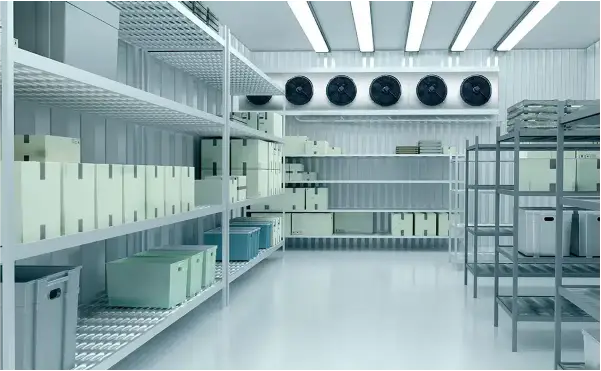
Product placement and storage clearances are considered with the required operating conditions.
Raw Material Storage
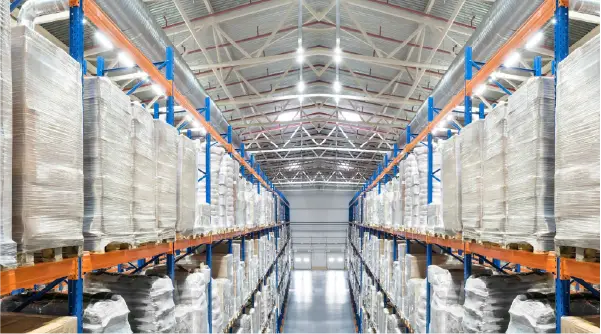
Storage requirements follow the material supplier’s instructions and the facility’s procedures.
Temperature Monitoring, Alarms and System Options
Include monitoring requirements in the initial project brief. Recording intervals, sensor accuracy, calibration, alarm limits and notification routes should be agreed before equipment is ordered.
- Temperature records: define the recording method, retention period and access required by your quality team.
- Alarm response: specify who receives notifications and the response expected when conditions move outside the agreed limits.
- Continuity requirements: request an assessment of standby refrigeration, backup power interfaces or other measures according to the consequences of downtime.
- System integration: identify any required connection to building controls, remote monitoring or an existing data system.
The selected functions, equipment and responsibilities are confirmed in the quotation and technical scope.
Why Choose TunelGroup for Pharmaceutical Cold Rooms?
- Coordinated manufacturing scope: cold-room panels, doors and refrigeration equipment can be considered together.
- Project-specific selection: the design starts with your product requirements, location and operating conditions.
- Defined supply scope: review the included equipment, requested options and installation responsibilities in one proposal.
- Technical discussion: use room plans and a clear operating brief to resolve layout and equipment questions before production.
From Project Brief to Handover
- Requirements: provide product details, temperature range, dimensions, quantity and site information.
- Design review: review the layout, panel and door selections, refrigeration duty and requested controls.
- Scope and production: approve the technical proposal, drawings, supply responsibilities and delivery arrangements.
- Installation and acceptance: agree the installation scope, commissioning checks and project acceptance criteria.
Temperature mapping examines how temperature varies across a storage area and can identify warmer or colder locations. Discuss the mapping protocol, operating conditions and acceptance responsibilities with the facility’s quality team. See the WHO guidance on temperature mapping of storage areas.
Pharmaceutical Cold Room: Frequently Asked Questions
What temperature should a pharmaceutical cold room maintain?
The required range comes from the particular product’s approved storage instructions. Provide the target conditions and allowed variation when requesting a quotation.
Can monitoring and alarms be included?
Request the required recording, alarm and notification functions in your brief. Their equipment, availability and scope are confirmed during the technical review.
What documentation should be agreed for the project?
Agree equipment documentation, operating instructions, test records and any qualification or mapping deliverables with the responsible quality team. Record who supplies and approves each item.
What information is needed for a quotation?
Send the product category, required temperature range, room dimensions or storage capacity, project location, loading pattern and requested monitoring or continuity functions.
Pharmaceutical Cold Room Price and Quotation
The price of a pharmaceutical cold room depends on the usable size, design conditions, panel and door specification, refrigeration duty and agreed control options. Delivery, installation and documentation requirements also affect the project scope.
Send your room dimensions, temperature range and project location using the form below. TunelGroup can review your requirements and prepare a project-specific proposal.


